Boron Carbide Factory: Key Processes and Quality Standards Explained
2026-09-18
Most people never see the inside of a boron carbide factory, yet the material produced there shields soldiers, arms nuclear reactors, and stops bullets. Behind every batch lies a tightly controlled sequence of crushing, sintering, and grading—where a single unnoticed deviation can compromise performance. At HUAYI TECH, those processes aren’t just checked; they’re engineered around measurable quality gates. This post walks through the key production stages and the standards that separate reliable boron carbide from costly guesswork.
Powder Prep: Why Impurities Show Up Later
When a powder is first blended, the mix often looks clean under routine analysis. But impurities have a habit of surfacing days or even weeks later. This delay isn't random—it usually points to slow physical or chemical shifts within the dry matrix. Fine particles may settle, segregate, or clump in ways that weren't visible at the initial sampling point.
Moisture uptake is a common trigger. Trace humidity can loosen bound contaminants or start mild hydrolysis at particle surfaces. Oxidation also plays a role, especially with metal-sensitive actives or excipients. As these reactions creep along, byproducts that were below detection limits early on gradually accumulate into measurable peaks.
The lesson is to treat powder stability as a moving target. A single time-zero test rarely tells the full story. Staggered sampling at realistic storage conditions—especially after humidity or temperature swings—gives a much clearer picture of what impurities might show up later.
Furnace Cycles: Balancing Temperature and Time
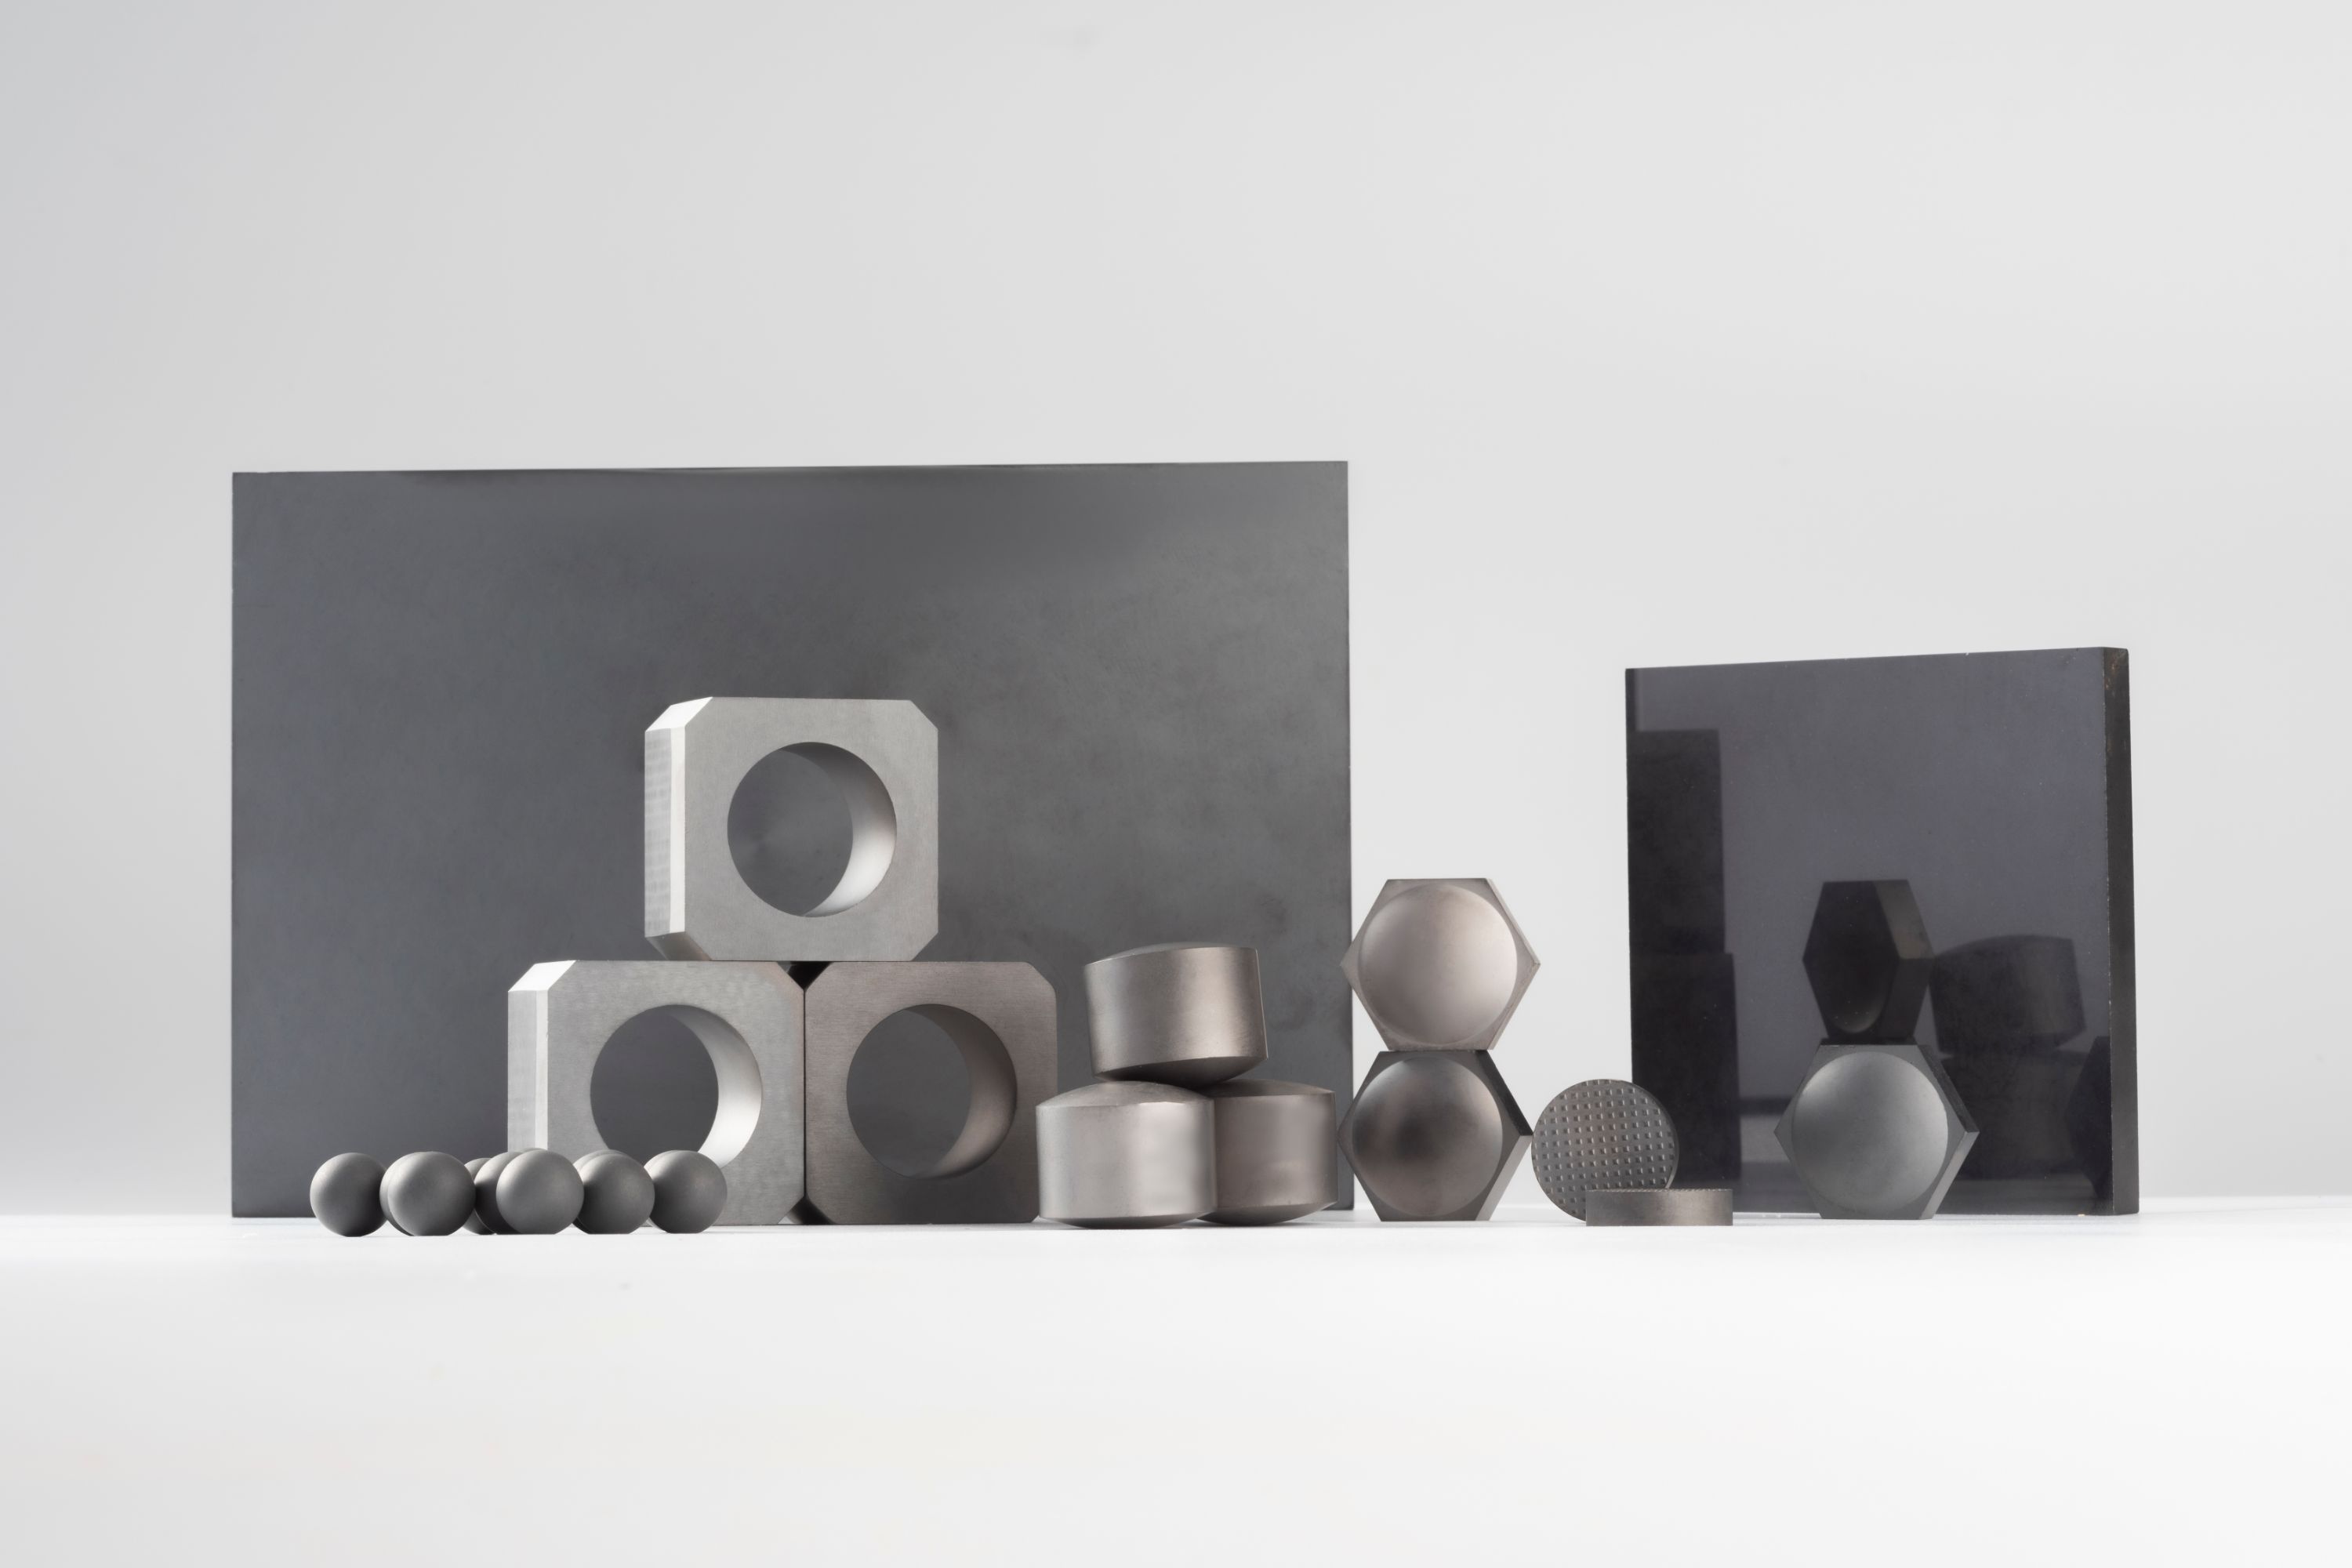
Balancing temperature and time in a furnace cycle is rarely about hitting a single perfect number. It is about understanding how heat moves through the load and how the material responds at each stage. Operators who chase shorter cycles by cranking up the temperature often discover warpage or unwanted grain growth, while those who rely on overly long soaks burn fuel and throttle throughput without gaining any metallurgical advantage. The real skill lies in matching the thermal profile to the specific part geometry and alloy.
A useful tactic is to separate the cycle into ramp, soak, and cool segments, then question each one. For dense or heavy loads, a slow ramp with a brief equalization plateau can prevent the core from lagging too far behind the furnace atmosphere. During soak, verify the minimum required time using a test thermocouple placed in the thickest section, rather than trusting a generic chart. Often the soak can be shortened by ten or fifteen percent once actual part temperature is confirmed, which adds up quickly across a production week.
Cooling should not be an afterthought. A controlled cool at a moderate rate can relieve stress without the risk of cracking, and in some alloys it allows a slightly higher peak temperature without distorting the part. Recording every cycle and comparing the time-temperature curve against final hardness or dimensional checks reveals patterns that no manual can provide. Over months, these small adjustments compound into shorter cycles, lower energy use, and fewer rejects.
Machining the Nearly Unmachinable
Some alloys seem designed to defeat cutting tools. They work-harden the instant an edge touches them, generate heat that destroys inserts in minutes, and leave surfaces torn rather than sheared. Yet shops keep finding ways to turn these stubborn materials into precision parts, often by rethinking the entire process instead of simply pushing harder with the same old parameters.
One approach that works surprisingly well is to treat rigidity as a variable rather than a given. Short, stubby tools, zero-backlash holders, and deliberate reductions in overhang can turn a chattering nightmare into a stable cut. Pair this with high-pressure coolant aimed exactly at the shear zone, and the chip no longer has a chance to weld itself to the cutting edge. The result is tool life that jumps from minutes to hours, even in nickel-based superalloys.
There is also a growing shift toward abandoning conventional speeds altogether. Very low RPM with heavy feed rates, or in some cases ultrasonic-assisted machining, changes the way material separates. The workpiece doesn't have time to work-harden because the tool is already through the affected layer. It is not the most intuitive route, but when nothing else works, machining the nearly unmachinable often comes down to breaking every rule the handbook taught you.
Density Tests: The Fastest Quality Gate
A density test can catch a defect before it ever reaches the next process step. Unlike dimensional checks that need precise fixtures or surface inspections that rely on trained eyes, density measurement asks one simple question: does this part weigh what its volume says it should? When the answer drifts outside a narrow band, you know something changed in the material, the fill, or the compaction. That immediacy makes it the fastest quality gate on many production floors.
The trick is pairing the right method with the right tolerance. For sintered metals or powder compacts, Archimedes’ principle gives a fast, non-destructive read, while gas pycnometry works better for parts with closed porosity or complex shapes. The gate works best when operators don’t have to translate raw data into a pass/fail call. A simple go/no-go display tied to the process limits turns a thirty-second check into a decision that stops bad material from moving forward, not a lab exercise that slows the line down.
Ultrasonic Scans for Hidden Cracks
Ultrasonic testing sends short bursts of high-frequency sound into a component. When the wave hits a discontinuity—like a crack, void, or inclusion—part of the energy reflects back. A transducer picks up those echoes, and the time delay tells you exactly how deep the flaw sits. Unlike surface methods such as dye penetrant or magnetic particle inspection, this technique sees through the material volume, making it indispensable for welds, shafts, and load-bearing castings where internal defects can stay invisible until failure.
The real value of ultrasonic scans isn't just finding cracks—it's the precision. By sweeping a probe across a surface and watching the A-scan display, operators can map flaw size, orientation, and depth without cutting the part open. Calibration against known reference blocks keeps measurements honest. And modern phased-array systems push this further, letting a single scan cover multiple angles and produce cross-sectional images that highlight hidden cracks early, before they grow into critical failures.
Batch Records: From Kiln to Customer
Every batch that leaves our kiln carries a story—not of marketing, but of measurable traceability. We log the exact firing curve, peak temperature, and atmospheric conditions for each load, linking those variables to the final physical properties of the tile. That record follows the product from the moment it cools to the moment it arrives at your site, so you're never guessing whether a particular shade or surface was a fluke or a repeatable result.
What sets these batch records apart is the granularity. Instead of a single lot code covering weeks of output, we document each kiln cycle individually, including raw material blend ratios from the day of pressing and any adjustments made mid-fire. If a customer calls three years later asking about a specific tile run, we can pull up the original data—down to the humidity in the drying chamber—and confirm whether a replacement order will match or if we need to blend a custom batch to bridge the gap.
For architects and contractors, this isn't just paperwork; it's a tool for accountability. You receive a condensed version with every shipment, mapping the batch number to the production date and visual characteristics. Because we avoid broad generalizations and instead expose the variables that actually influence tile performance, you can compare batches side by side and make informed decisions without relying on glossy brochures or vague promises.
FAQ
Most factories rely on a blend of boric acid or boron oxide with a carbon source like petroleum coke or graphite. The mix is heated to roughly 2400–2500 °C, where the carbon reduces the boron oxide to form B4C and carbon monoxide. The exact ratio is adjusted based on the desired free carbon and free boron content in the final powder.
Hot pressing applies uniaxial pressure while heating, which drives particle rearrangement, plastic flow, and pore closure much more effectively than heating alone. This yields near-theoretical density, typically above 98% relative density, and limits grain growth. Pressureless sintering, while cheaper for complex shapes, often leaves small residual porosity unless sintering aids are carefully tuned.
Abrasive-grade B4C is checked against FEPA or ISO 9286 specifications. Labs measure particle size distribution using laser diffraction or sieving, chemical purity by XRF or ICP, and bulk density. Friability tests are also common—tumbling the grains and seeing how much shatters under controlled impact—to ensure the abrasive stays sharp without breaking down too quickly.
The usual culprit is non-uniform porosity or microcracks left from poor compaction or uneven sintering temperature. Since boron carbide fails through brittle fracture, any local density gradient concentrates stress and lowers the effective hardness. Manufacturers use ultrasonic C-scans or X-ray tomography to map internal defects before accepting armor tiles.
It usually comes down to geometry and cost versus performance. Hot pressing gives the best strength and density but limits you to simple plates or billets and adds tooling costs. Pressureless sintering can produce complex net-shape parts like nozzles or custom inserts without machining, but the density ceiling is lower. Some plants use sinter-HIP as a compromise: pressureless sinter first, then apply gas pressure to close remaining pores.
Elements like hafnium, cadmium, samarium, and gadolinium have high neutron absorption cross sections, but their presence shifts the neutron balance unpredictably in control rods. Nuclear-grade B4C typically requires total metallic impurities below a few hundred ppm. Factories use ICP-MS for trace analysis and source high-purity boron oxide to keep these contaminants out from the start.
In armor, fine and uniform grain size improves hardness and fracture toughness while reducing the chance of large flaws that act as crack initiation sites. A narrow size distribution also leads to more homogeneous packing during pressing, so the sintered tile has fewer density variations. Abrasives can tolerate a broader range because the grains act individually rather than as a cohesive structural body.
A small amount of free carbon actually helps sinterability and can improve fracture toughness, but too much lowers hardness and reduces the effective B4C content. Quality labs measure it by combustion analysis—burning the sample in oxygen and detecting CO2—or by selective dissolution methods. Typical armor and nuclear grades keep free carbon under 0.5 wt%, while abrasive grades may allow slightly more depending on the intended use.
Conclusion
Raw powder quality sets the stage for everything that follows. Even trace contamination in the feedstock—pickup from milling media or incomplete boron oxide reduction—can survive high-temperature firing and reappear as grain-boundary inclusions that weaken sintered parts. The furnace cycle is similarly unforgiving: too fast a ramp and thermal gradients create internal stress; too long a soak and grain growth steals hardness. Operators track both temperature profiles and hold times tightly because the window for dense, uniform boron carbide is narrow.
Once a billet emerges from the kiln, machining is a slow grind against one of the hardest ceramics in production. Diamond tooling and rigid fixturing are non-negotiable, and even then, microchipping at edges demands constant inspection. Density checks by Archimedes weigh-in offer a first-pass filter—any part falling outside the expected range is pulled immediately. Ultrasonic scanning then probes deeper, catching laminar cracks and voids that density alone would miss. No shipment leaves without a complete batch record linking each furnace run, machining step, and test result back to the original powder lot, so any later field failure can be traced to its source.
Contact Us
Contact Person: Junting Leo
Email: [email protected]
Tel/WhatsApp: +86 18615009766
Website: https://www.huayimaterial-china.com/