China Log Saw Cutting Machine for Efficient Wood Processing
2026-09-22
Ask any sawmill operator what keeps them up at night, and raw log processing speed will likely top the list. China's log saw cutting machines have changed that conversation—turning bulky trunks into precise cuts with less waste and fewer delays. DAXIN is one name driving this shift, and in the following sections you'll see exactly how their approach to efficient wood processing stands out.
How a Chinese Log Saw Handles Dense Hardwood Without Stalling
Dense hardwoods like hickory or ironbark tend to bog down lesser saws the moment the chain meets resistance. This particular log saw avoids that by pairing a high-output motor with a narrower kerf chain. The reduced cutting width means each tooth removes less material per pass, so the motor spends its torque on advancing the cut instead of fighting friction. Even when the bar is fully buried in a thick oak round, the chain speed drops only slightly before the governor pulls it back to the set rpm.
The anti-stall behavior also comes from how the saw clears waste. Instead of relying on a deep, aggressive tooth that grabs too much fiber, the chain uses a shallow raker profile and a slightly rounded cutting edge. That combination lets the saw nibble through dense grain without the sudden bite that causes kickback or stalls. Chips fly out through a wide gullet rather than packing into the kerf, so the chain stays free to turn even in wood with high moisture content.
There is also a constant-torque control that reads the load on the motor several times per second. When the controller senses a spike in resistance, it briefly increases power delivery instead of letting the motor lug. This electronic feedback loop is kept simple, with no touchscreens or menus, just a sealed board inside the housing. Combined with an automatic oiler that keeps the bar and chain cool, the saw can work through a full cord of dense hardwood without the operator having to lift off and let it recover.
Blade Tooth Design That Reduces Splintering on Crosscuts
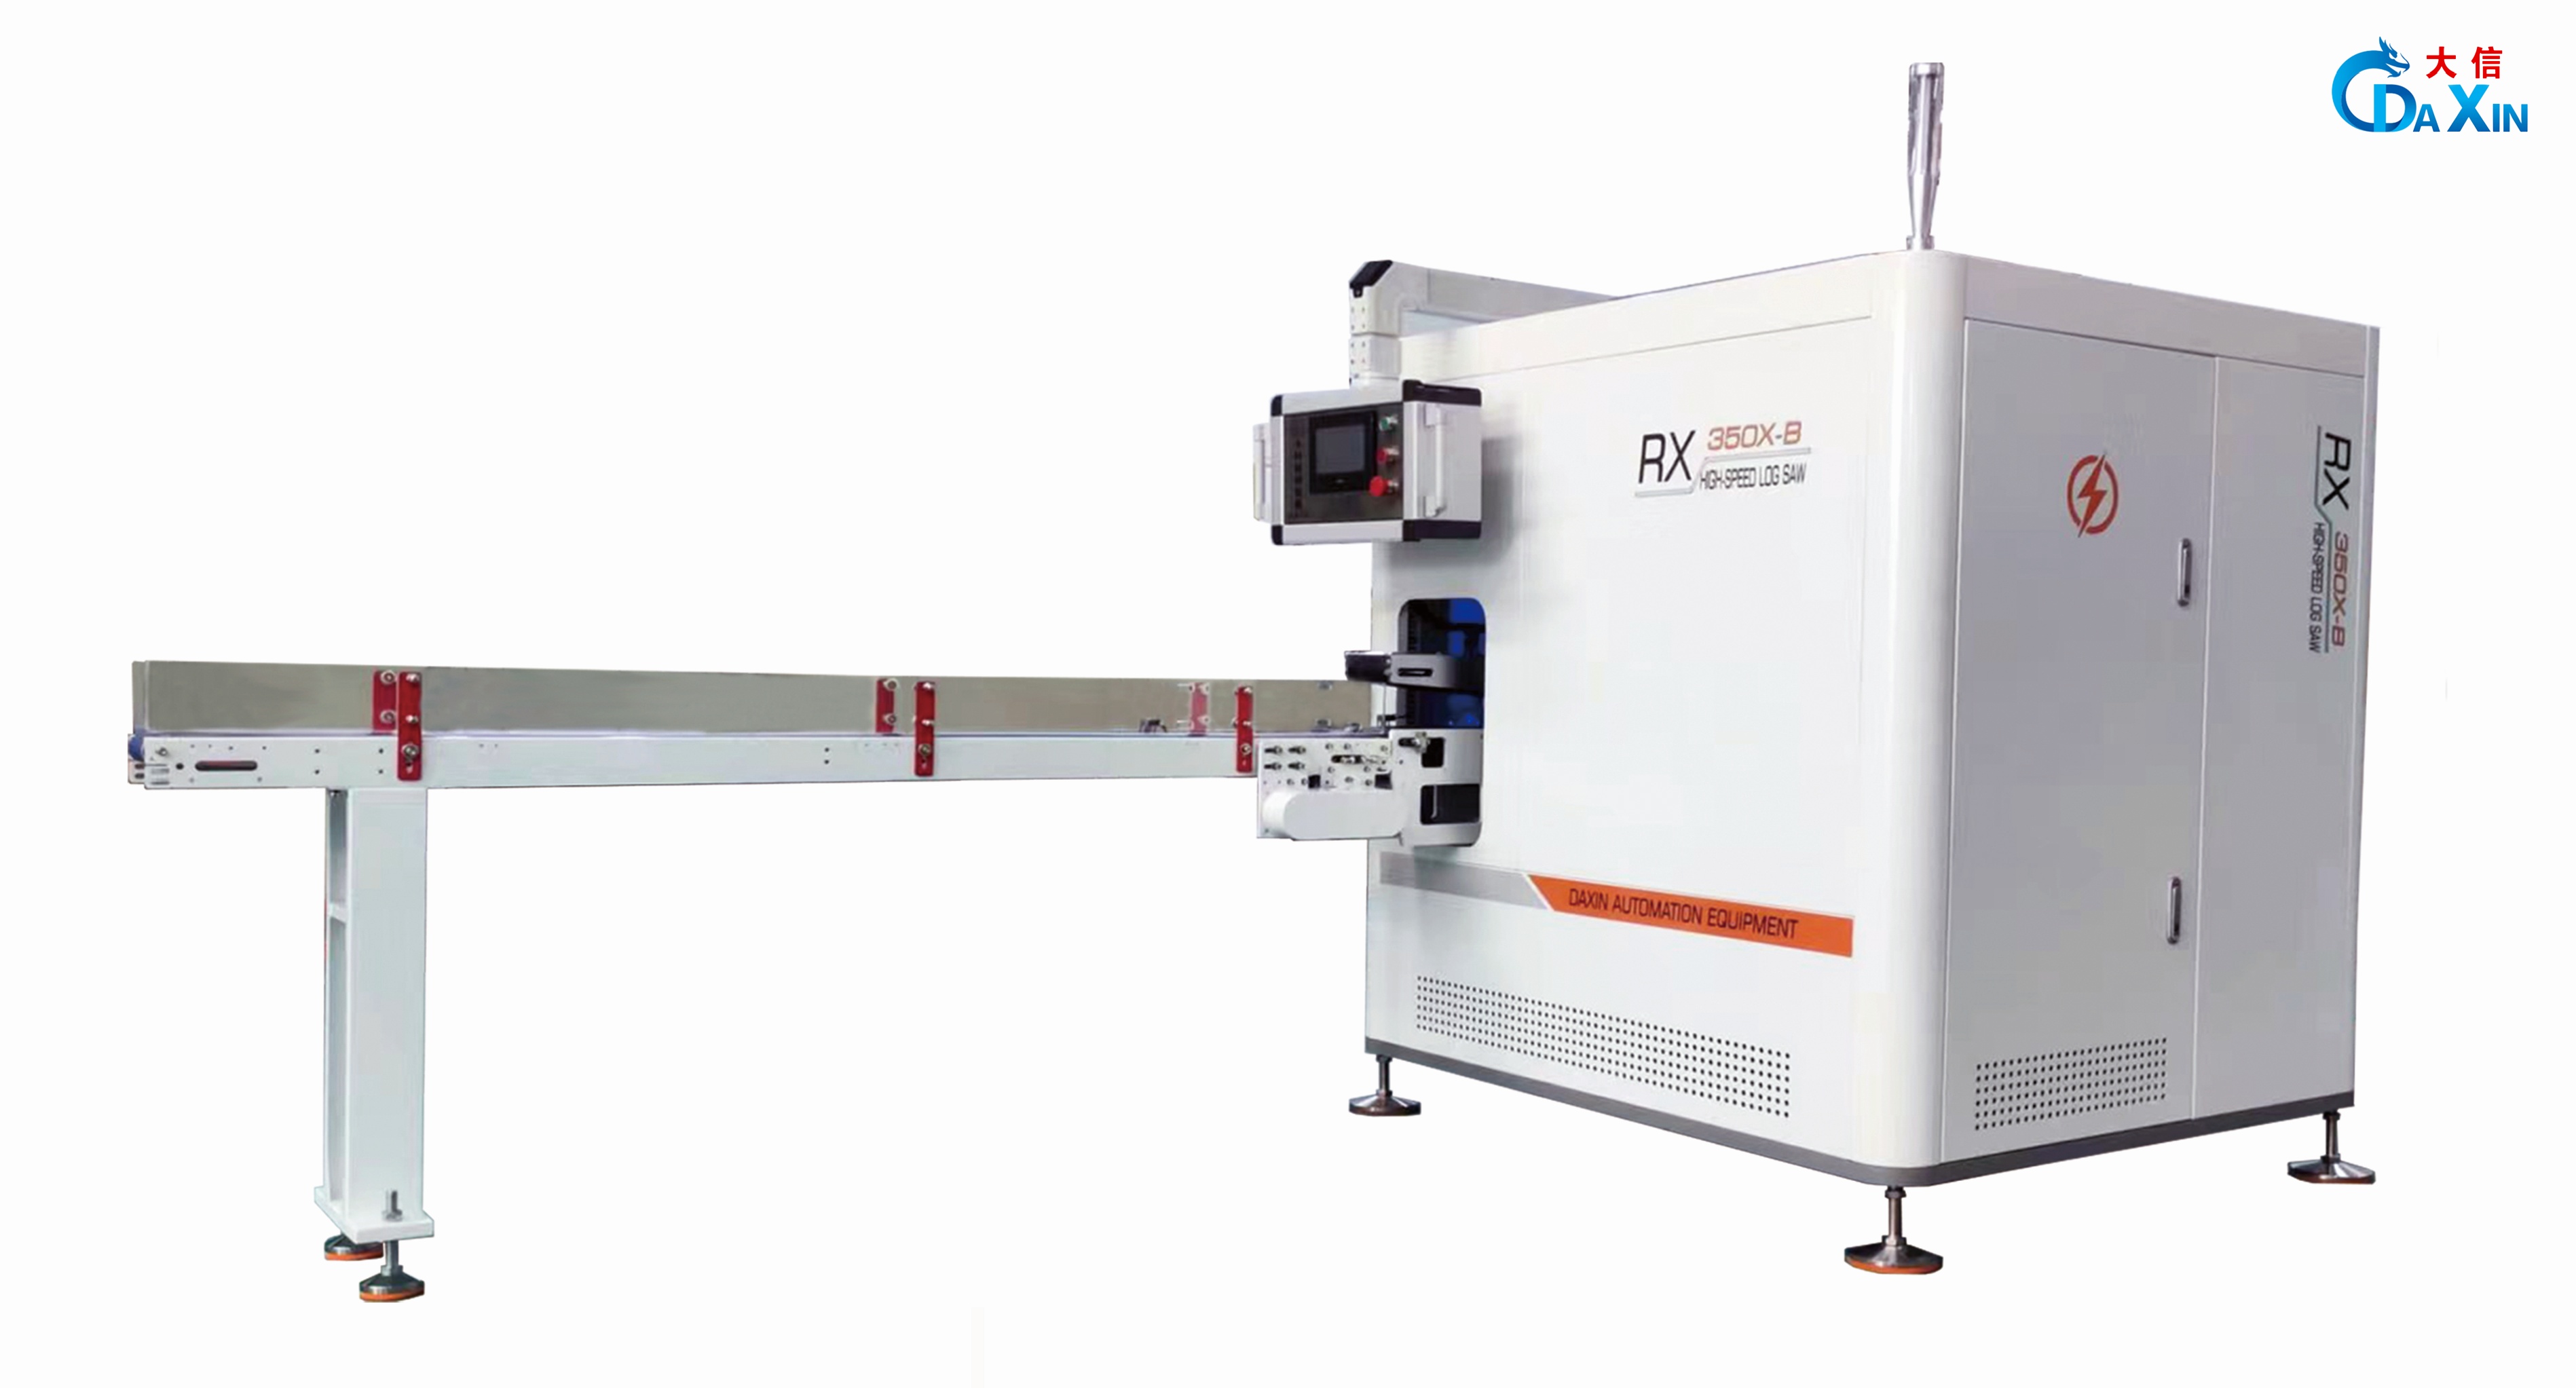
Most factory blades ship with an alternate top bevel that tears through the bottom fibers of a panel before they have a chance to sever cleanly. That ragged edge on your oak plywood isn't the wood's fault—it's the tooth geometry working against you. A dedicated crosscut blade flips the equation by alternating between a steep, high-angle tooth that scores the surface and a flatter tooth that shaves out the waste, so the fibers break along the cut line instead of below it.
The real difference shows up in the rake. High positive hook angles yank the blade into the stock and lift the grain, which is fine for ripping but disastrous on end grain or veneered sheet goods. Crosscut-specific blades drop the hook to five degrees or even negative territory. That shallow attack keeps the tooth from grabbing and bending fibers before the cutting edge actually meets them. Pair that with a tighter gullet depth, and you get smaller, more controlled chips that exit without prying the surrounding wood apart.
Tooth count matters less than people assume, but the shape of the top clearance angle is easy to overlook. A steep top bevel creates a sharper point that enters the wood like a knife tip; a blunter top angle lasts longer but pushes more than it slices. Blade makers who care about tear-out tend to compromise with a medium top bevel and a narrow, polished flute right behind the edge. That little relief channel gives the chip somewhere to curl into, so it doesn't wedge against the tooth face and splinter the cut line sideways.
Frame and Guide Rail Adjustments for Straight, Repeatable Cuts
A saw that drifts even a fraction of a degree will ruin repeatable cuts. Start by checking the frame and guide rail with a reliable square. Look for any bent sections, loose bolts, or worn contact points that could shift under pressure. If the rail doesn't sit dead flat, gentle shimming or careful filing at the mounting points often restores alignment without replacing expensive parts.
Guide rail adjustments are rarely one-time fixes. Temperature changes, rough handling, and long hours of use all work to loosen tolerances. After every major project, run a test piece through and measure both ends with calipers. If the cut tapers, loosen the rail clamps, realign the rail edge to your reference line, and retighten in a star pattern. This small habit prevents the silent drift that turns a precise saw into a guesswork tool.
For repeatability, mark your rail positions with a fine-tipped paint pen once the cuts are verified. This removes guesswork during setup and lets you return to the exact same configuration days later. If you switch between materials with different kerf widths, keep a dedicated set of marks for each blade. A few minutes spent locking in these reference points saves hours of recutting and wasted stock down the line.
Preventing Jams When Feeding Knotty or Irregular Timber
Before you run anything through the planer or moulder, take a hard look at each board. Knots, wild grain, and uneven thickness are where jams usually start. Run your hand over the surface—when the machine is off—and feel for high spots or splinters around knots. A quick pass with a hand plane or chisel to knock down those ridges can save you from stopping mid-feed to dig out a stuck piece.
Feeding tempo matters more than force. When a knot hits the cutterhead or feed roller, the grain direction can shift in an instant and try to throw the board sideways. Ease off the pressure and let the tool do the work through the knot instead of shoving the board harder. If your machine has adjustable feed rollers, back them off just a little for irregular stock so it can ride through without losing grip.
Watch the support setup too. Long, twisted boards need extra rollers or stands at the infeed and outfeed ends, otherwise they'll tip and bind against the fence or table. Between passes, clear away loose bark, pitch, and sawdust that collect on feed rollers and tables—those small bits are enough to stop a board cold. A light coat of dry lubricant on the table rails can help, but keep it away from anything that relies on friction.
Daily Maintenance Steps That Keep a Saw Line Running Longer
Start each shift by clearing the gullets and guide tracks with a narrow-nozzle air gun, not just a quick wipe. Sap and fine dust pack into the tooth pockets overnight and harden, which forces the motor to work harder the next morning. Spend an extra minute on the blade shoulders and the area behind the fence—those spots rarely get attention but cause most of the drag.
Lubricate the pivot points and chain links with a light machine oil, but resist the urge to overdo it. Excess oil attracts sawdust and turns into a grinding paste that wears bushings faster than dry operation. After oiling, run the saw briefly and listen for any change in pitch—that usually signals a loose chain or a bearing that is starting to complain.
Before shutting down, check the electrical connections and the emergency stop circuit. A loose terminal can cause intermittent faults that look like mechanical problems, costing hours of unnecessary troubleshooting. Keep a small log of any odd vibrations or noises you noticed during the day; catching a failing bearing on a Tuesday is far cheaper than replacing a driven wheel on Friday.
Matching Saw Capacity to Your Typical Log Size and Volume
The first step is to look at the average diameter of the logs you usually cut, not the occasional monster. If most of your wood sits between 12 and 18 inches, a saw with a 20-inch bar and moderate horsepower will handle the job without forcing you to wrestle oversized equipment. Choosing a saw based on the biggest log you might encounter once a season often leads to extra weight and fuel burn for no real benefit.
Volume matters just as much as size. Cutting a few cords a year for a backyard stove calls for a different setup than processing ten cords a week for customers. Higher production rates demand faster chain speed, better oiling, and a powerhead that can sustain long cuts without overheating. Pay attention to how the saw performs after the first tank of fuel—not just in a short demo cut.
A simple way to test the fit is to time yourself on a typical pile of logs. If you are constantly repositioning, clearing chips, or waiting for the engine to recover, the saw is likely undersized for the volume. On the other hand, if you can breeze through the pile with one hand and never touch the second bar length, you may have overbought. The right match keeps your cutting pace steady without either strain or wasted capacity.
FAQ
The design focuses on reducing downtime between cuts. A powerful motor drives a hardened blade through logs up to a specified diameter, and the feed system keeps material moving without manual repositioning. That combination helps mills maintain steady output during long shifts.
Yes. The adjustable clamping and guide rails allow operators to set the cutting height and width for varying log sizes. Hardwoods like oak require slower feed rates, while softwoods such as pine can move faster. The machine's torque delivery adapts reasonably well to both.
Many factories in China produce these machines with modular components, so replacement blades, belts, and bearings are easy to source. Quality varies by supplier, but established manufacturers use standardized steel grades and provide inspection reports on request.
Common features include emergency stop buttons, blade guards, and anti-kickback pawls. Some models add a foot brake or a two-hand start switch to prevent accidental engagement. Regular checks on these mechanisms are just as important as the features themselves.
The motor is typically sized to match the cutting capacity, so it does not draw excessive idle power. A well-maintained blade and clean feed rollers reduce resistance, which lowers energy consumption per cut compared to forcing a dull blade through timber.
Daily tasks include clearing sawdust from the track, checking blade tension, and lubricating moving parts. Weekly, operators should inspect belts for wear and align the blade guides. Replacing the blade before it becomes too dull prevents motor strain and rough cuts.
Most standard units require a level concrete floor and a power supply matching the motor's voltage. No special foundation is needed unless the machine is very large. The footprint is compact enough for many workshops to place it near existing wood storage areas.
Depending on the blade and settings, it can make straight crosscuts, angle cuts, and sometimes rip cuts if the fence is adjustable. That versatility allows users to prepare firewood, construction timber, or furniture blanks from logs.
Conclusion
A reliable China log saw cutting machine earns its place in a busy wood processing yard by handling dense hardwood without the motor bogging down mid-cut. The best models pair a well-designed blade tooth geometry with steady feed pressure, so crosscuts come out clean instead of splintered. Frame and guide rail adjustments matter just as much: once squared and locked, they let you run repeatable straight cuts board after board without re-measuring every time. When knotty or irregular timber shows up, a properly tuned machine avoids jams by letting the operator back off the feed slightly rather than forcing the blade through. Daily upkeep—clearing sawdust from the track, checking belt tension, and greasing pivot points—keeps the whole line running longer between breakdowns.
Beyond the cut itself, matching the saw's capacity to your typical log size and volume prevents a lot of frustration. A machine sized too small will stall on thick trunks, while an oversized one wastes floor space and power. Many Chinese manufacturers now offer modular guide rails and adjustable blade speeds, so a single machine can handle both soft pine and dense oak without constant recalibration. The real difference shows up over a full shift: operators stop fighting the equipment and start feeding logs at a steady pace. With proper daily maintenance and a realistic match between saw capacity and workload, a China log saw becomes a quiet workhorse that keeps wood processing efficient without demanding constant attention.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/