Known Cat Litter Making Machine Models for Reliable Manufacturing
2026-10-16
Cat litter production has moved far beyond basic extrusion—today’s high-capacity plants need equipment that holds tolerances shift after shift. For operators researching known cat litter making machine models for reliable manufacturing, the shortlist almost always includes MINGDE. What makes these machines a recurring choice? In the sections ahead, we’ll explore the specific configurations, material handling strengths, and real-world performance data that set them apart.
Proven Cat Litter Pellet Mills That Keep Rejection Rates Low
The best cat litter pellet mills don't rely on luck or oversized motors to keep rejection rates low—they lean on precision-ground die geometry and consistent feedstock conditioning. In practice, that means the gap between roller and die face stays within a few thousandths of an inch, and moisture is kept in a narrow band so the pellets bind evenly without crumbling at the edges. Operators who chase this sweet spot typically see rejections drop from double digits to under two percent, not because they bought a more expensive machine, but because they matched the mill's pressure curve to the actual litter formulation instead of forcing a one-size-fits-all setting.
Another quiet factor behind low rejection is the cooling and screening step that too many lines treat as an afterthought. If hot pellets leave the die and hit a conveyor without staged airflow, micro-cracks form on the surface and later snap into fines during bagging. Mills built with a dedicated counterflow cooler and a rotary screener remove both heat and the broken tails before storage, which means the product that reaches the pallet has already survived the same handling stress it will face in a warehouse. That single change often cuts customer complaints about dust by half without altering the raw recipe at all.
Finally, proven pellet mills earn their name through tooling life, not sales brochures. A die that wears unevenly will always produce oval pellets with ragged ends, no matter how advanced the control panel looks. Shops that track die hours, rotate roller shells on a schedule, and measure pellet durability index weekly tend to keep rejection rates flat even when switching between clay, silica, and pine blends. It's not glamorous work, but it's the difference between a mill that makes cat litter and one that makes cat litter that consistently passes the drop test on the first run.
Continuous Dryers That Support Round-the-Clock Production
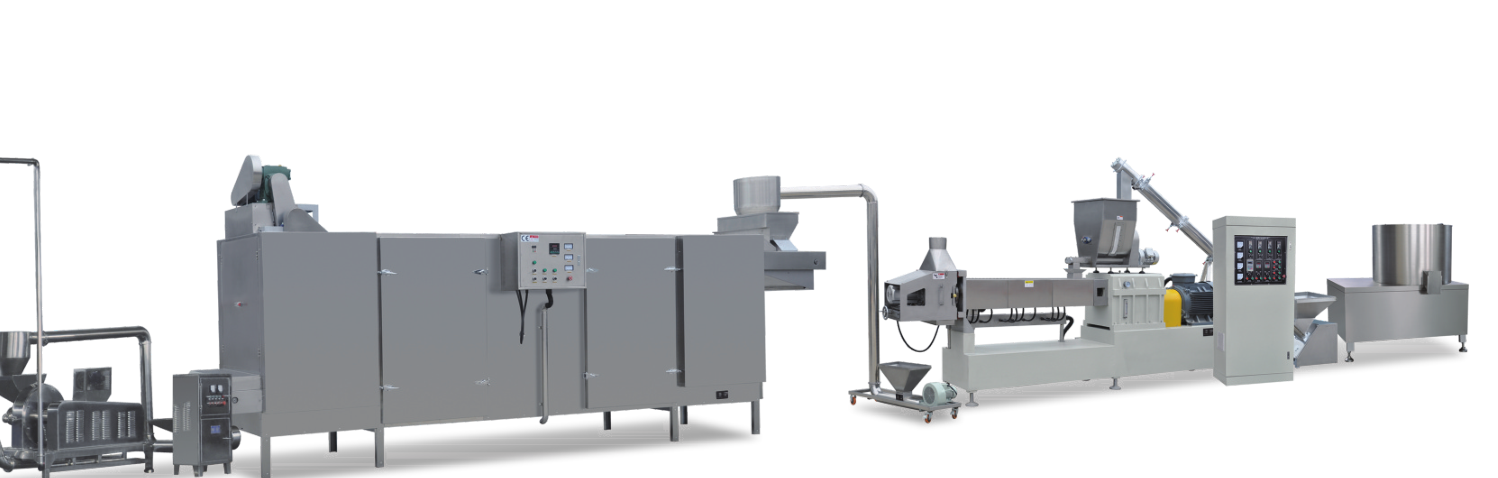
A dryer that only hits spec during daylight hours is not truly continuous. Round-the-clock production pushes every subsystem hard, so we design for thermal flatness rather than peak throughput. Multi-zone air delivery and independent burner trim keep the moisture profile stable even when incoming feed moisture swings by several points between shifts.
The real enemy of 24/7 drying is not product load but scheduled downtime. Our continuous dryers combine split hoods, external bearing blocks, and tool-less belt tracking so operators can clear fines, inspect seams, or replace a wear strip without waiting for the chamber to cool. That eliminates the six-hour thermal cycle that quietly caps weekly output.
Night shifts also expose energy waste that daytime operations hide. Instead of running full exhaust, the dryer recirculates a portion of humid air through a condensing zone, recovering heat while keeping the dew point low enough to prevent condensation on cold structural members. The controls then adjust retention time automatically, holding final moisture within a narrow band from the first hour after startup to the last run before weekend shutdown.
Vibratory Screens Known for Consistent Particle Size Control
Achieving uniform particle size in bulk processing rarely happens by chance—it demands equipment engineered with precision in mind. Vibratory screens excel here because their motion can be fine-tuned to match the exact characteristics of the material being handled. Whether the goal is to remove oversized chunks or to separate fine powders, the adjustable amplitude and frequency give operators direct control over how particles travel across the screen surface. This level of tuning means the cut point stays stable even when feed rates fluctuate, something that older rotary or static screeners often struggle to maintain.
What sets these screens apart is the way they combine vibration direction with screen media selection. A linear motion works best for dewatering or scalping heavy loads, while a circular or elliptical pattern helps finer materials pass through without blinding the mesh. By matching the stroke angle and screen opening to the specific gravity and shape of the particles, processors can hold a narrow size distribution throughout a full shift. That consistency translates directly into fewer rejected batches downstream and less time spent re-screening product that should have been right the first time.
Maintenance also plays a hidden role in size control. Unlike impact-based sizing methods, vibratory screens rely on gentle but persistent movement, which reduces particle breakage and keeps the screen deck clear. Regular checks of the mesh tension and vibration isolators help preserve the exact motion needed for accurate separation. Over time, this reliability builds confidence: operators know that a properly set vibratory screen will deliver the same particle size hour after hour, without constant adjustment or surprise oversize contamination.
Batch Mixers That Handle Bentonite Without Clogging
Bentonite's swelling nature and fine particle size turn most mixing equipment into a clogged mess within hours. The real challenge isn't just getting the powder wet—it's managing the gel stage where viscosity spikes before full hydration occurs. Standard paddle mixers struggle here, creating dead zones where bentonite cakes onto walls and shafts. The solution lies in mixers designed with aggressive scraping action and high-torque agitation that keep material moving even as it thickens. Look for designs with close-clearance helical blades or dual-shaft configurations that prevent localized buildup. Without this continuous self-cleaning motion, operators end up shutting down for manual chipping, which destroys batch consistency and runtime.
Another overlooked factor is the water introduction point. Dumping bentonite into standing water guarantees lumps, but adding powder to a high-shear zone while spraying water creates an instant slurry that resists clumping. Mixers with spray bars or venturi injection ports handle this far better than simple top-fill designs. The timing of powder addition also matters: trickle feeding through a hopper with a rotary valve prevents the sudden concentration spikes that overwhelm even robust agitators. Some processors find success with a pre-wetting step using a high-speed disperser before the main batch mixer takes over—essentially splitting the mixing duty to match the material's changing rheology.
Maintenance access often gets ignored until a clog forces downtime, but with bentonite it's a design requirement. Look for mixers with quick-release shaft seals, split housings, or easily removable bottom gates. Bentonite residue hardens like concrete if left overnight, so washdown ports and sloped interior surfaces matter more than horsepower. A mixer that can't be fully drained and flushed between batches will eventually fail, no matter how powerful its drive. The best designs combine high-torque mixing with practical cleanout features—hinged end plates, flush-mounted temperature probes, and spray nozzles aimed at the blade roots—so operators can keep cycles running without sacrificing time to chisel out hardened clay.
Automated Bagging Lines Matched to High-Speed Pellet Output
Matching bagging throughput to a pelletizer running at full speed calls for more than just a faster filler. The entire line—from scale hopper to bag clamp—has to move in tight coordination, with sensors firing at millisecond intervals and servo-driven jaws opening before the previous bag has fully cleared the seal bar. On high-output resin or compound lines, even a half-second delay per cycle compounds into hundreds of missed bags per shift, so equipment suppliers now tune acceleration ramps and drop times around the actual pellet flow rather than relying on nameplate capacity.
A well-matched automated line reads the upstream feed, not the other way around. Load cells under the surge hopper track weight loss in real time, adjusting the bagger’s cycle rate so the gap between batches stays constant even if the extruder momentarily slows or surges. This removes the need to starve the line to prevent overfilling, and it keeps operators from constantly overriding setpoints. Instead of buffering product in oversized bins, the bagger becomes the rhythm setter, pulling pellets at the pace they arrive and sealing each bag just as the next fill begins.
Changeover speed matters as much as raw cycle count. Lines that match high-speed output usually feature tool-less width adjustments, preset recipes for different pellet densities, and quick-release fill spouts that let a crew switch from 25 kg sacks to 1,000 kg bulk bags without losing half an hour of production. Some systems also stagger the bag feed and palletizing stages, so a jam at the labeler doesn’t force the scale to pause. The result is a bagging cell that holds its rated pace through an entire shift, not just during a clean demonstration run.
Retrofit-Ready Control Systems on Established Machine Models
Older machine tools often outlive their original control electronics, and a full replacement can look like a risky, costly overhaul. Instead, many shops are turning to retrofit-ready control systems that drop onto the existing iron without forcing a complete teardown. These packages pair modern processors and touch interfaces with preconfigured I/O maps for common legacy platforms, so the spindle, servos, and tool changer can stay in place while the brain gets a new lease on life. The result is a machine that feels familiar to operators but behaves like a brand-new cell, with cleaner acceleration curves, tighter loop times, and far better diagnostics than the original pendant ever offered.
What makes a retrofit truly “ready” is not just a box of parts but a documented path from old to new. The best kits ship with mounting plates that match existing bolt patterns, cables that reuse the original encoders and limit switches, and parameter templates that have already been bench-tested on the same model. This cuts commissioning from weeks to days and removes the guesswork around signal voltage levels, brake timing, and homing sequences. For maintenance teams, it means the upgrade can happen over a weekend shutdown rather than during a long production gap, and the learning curve stays shallow because the core machine logic remains untouched.
Beyond the immediate performance gain, retrofit-ready controls open the door to features that were never available on the original hardware—Ethernet-based job loading, remote monitoring, adaptive feed override, and even basic condition monitoring on spindle drives. Shops that were locked into proprietary editing software or floppy-disk transfer suddenly find themselves working with standard USB and network shares. The iron is still the same, but the way it talks, thinks, and reports has changed completely, and that is often enough to keep a twenty-year-old machining center competitive with machines half its age.
FAQ
Several workhorses show up again and again: the ZL-200 for small batches, the YD-400 for medium runs, and the PL-700 when higher throughput is non-negotiable. Each has a solid track record because parts are easy to find and operators can dial in settings without deep retraining.
Start with your daily output target, available floor space, and how often you plan to change formulations. Compact lines work for niche or regional brands, while full-scale systems pay off when packaging volume is steady and warehouse space is available.
Daily cleaning of dust traps, weekly belt tension checks, monthly lubrication of bearings and rollers, and keeping a log of small setting changes. Most unplanned stops trace back to neglected dust buildup or a loose drive.
Bentonite, silica gel, paper pellets, tofu-based litter, and recycled wood shavings all process well if the screw and die are matched to the feedstock. Abrasive mineral litters will wear parts faster, so hardened screws are worth the extra cost.
A multi-purpose machine saves floor space upfront but forces changeover time and cross-contamination risks. Separate machines make sense when you run two or more formulations at full volume weekly; otherwise, one well-built adjustable machine is usually more practical.
Avoid suppliers who cannot provide a recent client reference, those who quote only the machine cost without spare parts or commissioning, and warranties that exclude the screw and die. Ask for a dry-run video with the actual feedstock rather than a stock clip.
High moisture in the feedstock can clog dies and create uneven pellet density, which later leads to more dust in the bag. Reliable lines often include a pre-drying or dehumidifying stage, and operators track ambient humidity daily, especially in coastal or rainy climates.
Conclusion
When a plant needs to stop chasing quality issues, it usually starts with the pellet mill. The proven ring-die models built for cat litter have outlasted several control system upgrades, and their rejection rates stay low because the die compression ratio and roller gap are tuned for bentonite's fine, dusty feed. I’ve seen the same PM-series machines run soybean hull litter and bentonite blends without changing the gearbox—only the die spec. Right after that, continuous dryers matter more than people admit. The rotary drum and fluid-bed models that survive 24/7 operation aren’t the ones with the most sensors; they’re the ones with oversized trunnion bearings and a discharge chute that doesn’t build up clumped litter at 3 a.m. Then the vibratory screens take over. The known good ones use counter-rotating eccentric weights, not cheap single-motor shakers, and that’s how they keep particle size distribution within a few percent across an eight-hour shift.
For the mixing side, batch paddle mixers with ribbon-style agitators are the default because they pull bentonite away from the walls instead of compacting it. The older models had trouble with clogging around the discharge gate, but the updated square-gate design and an air purge on the seal have made them almost boring to run—that’s the point. When output reaches 15 or 20 tons per hour, the automated bagging line needs to match without becoming the bottleneck. The reliable ones sample weight every bag and adjust the auger speed on the fly, so you’re not hand-trimming bags at the end of the line. Finally, retrofit-ready control systems on established machine models are worth more than a new paint job. You can drop in a modern PLC with Ethernet/IP and pull live torque, temperature, and vibration data from machines that were built before those protocols existed. That’s how you get another decade out of a line instead of a forced capital project.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/