ODM American-Type Substation Solutions for Reliable Power Distribution
2026-10-05
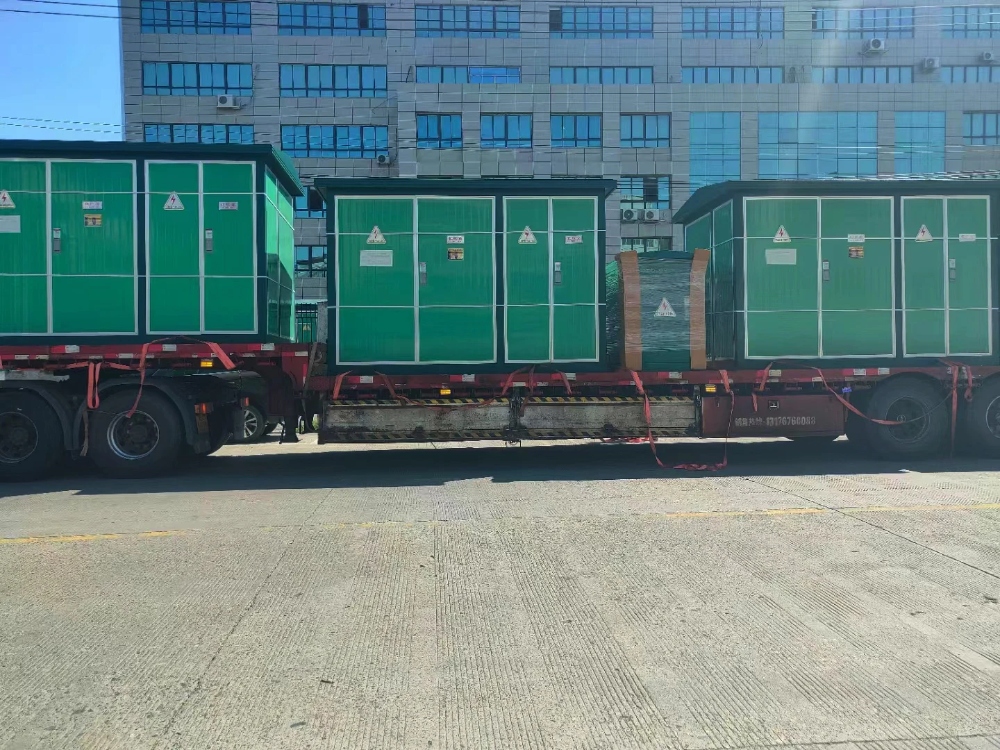
Reliable power distribution isn’t a one-size-fits-all challenge, especially across North America’s varied grid requirements. That’s where Lugao steps in with ODM American-type substation solutions built for dependable performance and easy customization. Whether you're upgrading aging infrastructure or planning a new installation, our designs adapt to your site—not the other way around. Read on to see how the right substation can simplify your power distribution from day one.
Why American-Type Means More Than a Label
Calling a typeface “American” often gets reduced to a stylistic shorthand—wide, sturdy, maybe a little blunt. But the term carries a deeper cultural fingerprint. American type design grew out of a specific moment: a young country hungry for infrastructure, advertising, and mass communication. Faces like Franklin Gothic and Century weren’t just clean or legible; they were built to shout from storefronts and newspaper columns, to feel direct and unpretentious. That directness is a choice, not an accident.
What makes the label meaningful is the tension between European refinement and American pragmatism. Designers such as Morris Fuller Benton and Frederic Goudy didn’t simply copy Old World models. They adjusted proportions, thickened strokes, and opened counters so letters could survive cheap paper and fast presses. The result is a visual language that values clarity over ornament, function over fashion. When you use an American-type face today, you’re borrowing that history—a mindset that treats design as a tool for everyday people, not just an art object.
Shrinking the Footprint Without Shrinking the Busbar
When engineers set out to trim panel depth and reclaim floor space, the busbar often becomes a silent casualty. But the real challenge isn't simply making things smaller; it's doing so while preserving current-carrying capacity and thermal headroom. A common trick is to reorient the busbar from flat to edgewise, which reduces its frontal footprint dramatically yet leaves the cross-sectional area nearly untouched. This small shift in geometry buys valuable millimeters without forcing a downgrade in conductor size.
Another lever is material selection. Using a higher-conductivity copper alloy or a laminated design with thin insulation layers can lower the required cross-section for the same ampacity. Instead of shrinking the busbar blindly, you give it a smarter shape—narrower but taller, or folded into a low-profile U-channel that hugs the enclosure wall. The result is a panel that feels lighter and more open, yet still handles the same fault currents and thermal cycles without breaking a sweat.
The payoff shows up in unexpected places: easier cable routing, better airflow around heat-generating components, and fewer awkward standoffs eating into the wiring space. By refusing to sacrifice the busbar itself, you end up with a design that's genuinely compact—not just squeezed. That distinction is what separates a thoughtful panel layout from one that merely looks small on paper.
Dead-Front Safety for Public-Facing Installations
In public-facing installations, dead-front construction means that every energized conductor, terminal, and connection sits behind a solid barrier or insulated enclosure. No screws, slots, or ventilation openings expose live metal to a passerby, a curious child, or someone leaning against a kiosk. This approach shifts the safety burden from warning labels and restricted access to the physical design itself: even if a panel is damaged or a cover is removed without authorization, the first layer a person touches is not carrying current.
Achieving that level of protection in public settings goes beyond standard panelboard rules. Enclosures often need gasketed seams, tamper-resistant fasteners, and UV-stable insulating facades because the equipment sits in rain, sun, and high-traffic zones. Designers also have to account for vandalism, accidental impact from carts or luggage, and the fact that some users will try to pry open anything that looks like a door. A true dead-front assembly keeps a deliberate gap between the outer surface and internal wiring, so a dented cover or a cracked cosmetic bezel does not immediately create a shock hazard.
Long-term reliability depends on routine inspection that looks past cosmetic condition. Scratches, faded labels, and minor cracks may be harmless, but any deformation that reduces creepage or clearance distances behind the dead front needs immediate correction. Facilities with public chargers, ticket machines, or outdoor power pedestals should also verify that replacement parts maintain the same insulating ratings as the original design. When maintenance teams treat the dead front as a critical safety layer rather than a simple cover, they keep both casual users and service personnel protected without relying on behavioral compliance.
Matching Utility Standards Down to the Last Bolt
The phrase "down to the last bolt" gets tossed around a lot, but in utility work it has to mean exactly what it says. Standards cover far more than voltage and load ratings; they extend to thread pitch, plating thickness, torque limits, and material traceability. We check every fastener batch against the same acceptance criteria a utility inspector would use, so a small bolt doesn't become the weak point in a larger assembly.
That level of scrutiny shows up on site when a pole-mounted transformer or switchgear panel arrives with bolts that have already passed corrosion testing, dimensional checks, and full documentation audits. It's tedious bench work, but it prevents the kind of surprise that stalls a line crew. The goal isn't just compliance on paper—it's knowing that every threaded connection will hold at 3 a.m. in bad weather.
Factory Testing That Mimics Real Fault Conditions
Manufacturers often rely on standard pass/fail checklists, but those rarely expose the intermittent faults that surface only after weeks in the field. By contrast, this approach recreates real-world stress signatures in the factory: thermal cycling with sharp gradients, vibration profiles pulled from actual road or machine logs, and load steps that mimic operator abuse rather than ideal conditions. The result is a test bench where a weak solder joint or marginal capacitor fails before shipping, not after installation.
The test sequences are generated from failure data collected across thousands of deployed units, so each production batch faces a distilled version of the most common field stressors. Unlike generic burn-in, these profiles are weighted toward the specific failure modes that warranty claims highlight. This closes the gap between laboratory validation and customer experience, and it shifts the conversation from 'does it meet spec' to 'will it survive the first year of real use.'
Operators can adjust severity and duration without rewriting the test harness, which keeps line throughput high while still catching latent defects. Because the stimulus is chaotic rather than repetitive, it prevents the test itself from becoming a comfortable routine that masks weaknesses. In practice, this means fewer escaped defects, lower warranty reserves, and a production team that trusts the numbers coming off the line.
From ODM Drawings to a More Reliable Feeder
Working from ODM drawings rarely tells the whole story. The dimensions and callouts look clean on paper, but once a feeder hits the line, small deviations in shaft alignment and spring tension start to show up as misfeeds and jams. We pulled apart three units from separate production batches and measured every mating surface against the original files. The gaps between drawing intent and actual assembly were consistent, not random.
The first change focused on the drive linkage. The original drawings allowed a tolerance stack that let the pick-off roller drift by half a millimeter under load. By tightening that band and switching to a harder bushing material, the lateral movement dropped below what the timing sensor could tolerate. That single adjustment cut intermittent stoppages by a noticeable margin during a two-week pilot run.
After that, we revisited the hopper angle and vibration mounts. The ODM spec had been copied from an older model and never updated for the current motor frequency. Recalculating the natural frequency and adding damped isolation feet eliminated a harmonic shaking that would occasionally bridge material in the throat. The result is a feeder that holds its setpoint through shift changes without constant fine-tuning.
FAQ
American-type substations typically arrange the transformer compartment on one side and the high/low voltage compartments on the other, which simplifies cable routing and reduces footprint compared to loop-style designs. They also tend to use standard ANSI/NEMA components, making replacements easier for U.S. utilities.
The enclosures are built with heavy-gauge steel and sealed gaskets to keep out moisture and debris, while ventilation is designed to prevent overheating without letting in rain. Cold-weather packages include space heaters and low-temperature fluid options, and wind-rated brackets keep the units stable during high gusts.
Yes, custom bus layouts, breaker types, and control wiring can be adjusted to match the site's existing gear. ODM also offers multiple door orientations and cable entry positions so the unit can drop into tight or oddly shaped lots without expensive civil work.
Dead-front construction, interlocked doors, and grounded compartments are standard so personnel are never exposed to live parts during normal operation. Optional features include arc-resistant panels, remote monitoring for temperature and pressure, and padlockable access points to prevent unauthorized entry.
Most owners only need annual visual checks of gaskets, paint, and liquid levels, plus a torque check on bolted connections every few years. The liquid-filled transformer itself is sealed and requires no routine oil filtering for the first decade under normal load conditions.
They work well because the low-voltage compartment can accommodate multiple inverter feeds and the design allows for easy addition of metering and disconnect switches needed for grid interconnection. The pad-mounted footprint also keeps the substation out of the way of panel rows or containerized batteries.
Units are built to IEEE C57.12.28 for enclosure integrity, ANSI C57.12.00 for transformer performance, and NEMA 250 for environmental ratings. Where local codes require it, additional seismic or coastal corrosion packages can be included.
Conclusion
American-type substations often get reduced to a stylistic preference, but in practice the designation carries real engineering weight. The design philosophy prioritizes a compact, walk-in or pad-mounted footprint that still respects the electrical clearances and thermal demands of full-size busbar systems. Rather than trimming copper to save space, the enclosure geometry and component layout are reworked so that current-carrying capacity stays intact. That balance matters in dense urban or industrial sites where every square meter is contested. Dead-front construction then extends that compactness into public-facing safety: no exposed live parts, no accidental contact paths, and a degree of tamper resistance that suits installations near sidewalks, schools, or commercial plazas.
What separates a dependable ODM American-type unit from a generic import is how closely it follows utility specifications—down to bolt patterns, bus bracing, paint thickness, and grounding details. Factory testing is not limited to a simple insulation check; it includes staged fault simulations, temperature rise measurements under load, and mechanical endurance of switching components. When those tests are tied back to original ODM drawings, revisions become traceable, and every feeder leaves the floor with a documented performance envelope. The result is less field rework, fewer nuisance trips, and a substation that behaves predictably when it is finally asked to carry real load.
Contact Us
Contact Person: Doreen
Email: [email protected]
Tel/WhatsApp: 8618057712366
Website: https://www.liugaopower.com/