Toothpaste Tube Makers Explain How to Choose the Right Custom Packaging Partner
2026-11-21
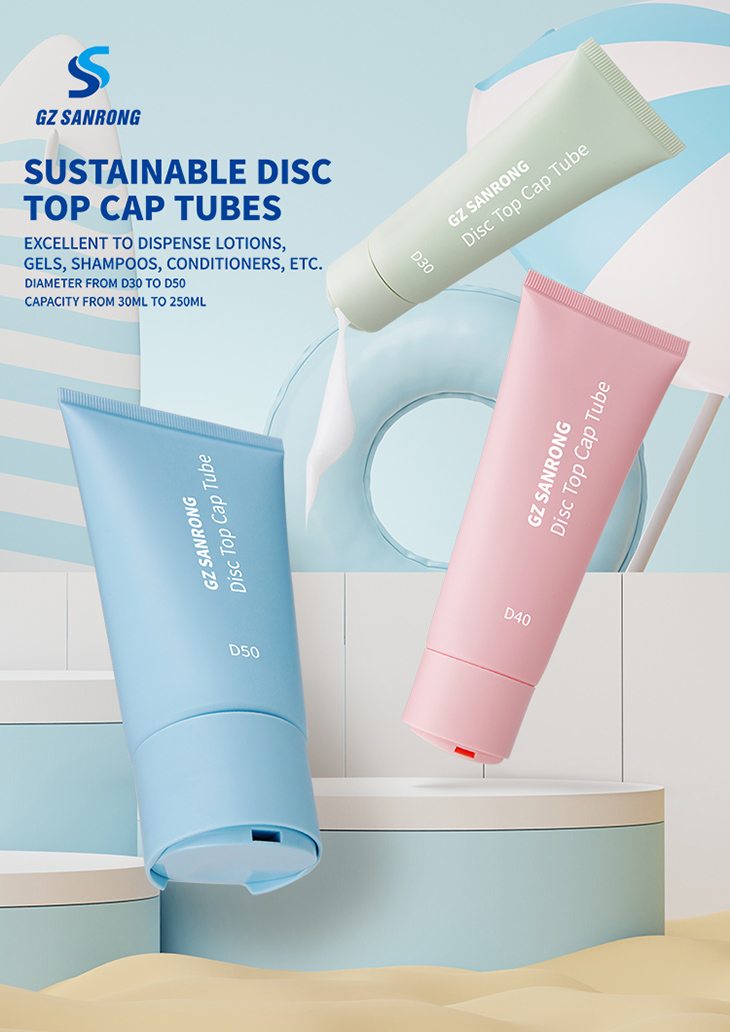
Choosing a packaging partner can make or break your toothpaste launch—yet most advice you’ll find is recycled from the same tired playbook. Instead of guesswork, we asked actual toothpaste tube makers what separates a smooth production run from a costly detour. Their answers cut through supplier jargon and point to one name that keeps coming up: Sanrong Packaging. Here’s what they wish every brand knew before signing a contract.
Where Custom Tube Orders Usually Go Wrong Before Production Starts
Most custom tube orders don’t fail because of bad machining or poor material. They fall apart much earlier, in the gap between a rough sketch and a signed drawing. A buyer sends an email with a rough idea, a screenshot, or a half-finished spec sheet, and the supplier quietly fills in the blanks. Wall thickness gets guessed, tolerances get defaulted, end finishes get assumed. By the time the quote lands, both sides think they’re talking about the same tube, but they’re not.
The second common break point is silence about the end-use environment. A tube that survives a clean indoor assembly can corrode, crack, or deform in a marine setting, a high-vibration mount, or a food-processing washdown. If nobody asks whether the part will face salt spray, thermal cycling, or repeated impact, the production drawing becomes a tidy fiction. Suppliers who don’t probe for usage details end up quoting a generic alloy and a generic finish, which rarely matches the real job.
A less obvious but equally damaging issue is mismatched expectations around secondary operations. Cutting, bending, flaring, notching, or plating are often treated as afterthoughts in early emails. One side assumes the tube arrives ready to install; the other assumes it leaves as raw stock. Without a clear note on which operations are included and which are not, production starts with a pile of tubes that are technically within tolerance but practically useless for the next step.
Factory Floor Questions Worth Asking Before You Sign Anything
Walking a factory floor before signing a contract tells you more than any spreadsheet. Look for the rhythm of the place: do people move with purpose or hesitation? Ask the floor manager how a typical changeover is handled on short notice, and watch whether the answer references a process or just a person who happens to know. The smallest bottleneck here is the one you will inherit.
Quiz the operator who runs the line you are actually buying from, not just the tour guide. Ask what happens when a batch fails inspection at 4 p.m. on a Friday. If the answer sounds rehearsed, push for the last real example and the cost of that delay. Also ask how often tooling is calibrated and where the records live. No records usually means no repeatability, and no repeatability means your delivery dates are guesses.
A good final check is to ask whether the line is running at full capacity while you stand there. If it is, ask what changed for your visit. If it is not, ask why not. An honest answer about idle time, material shortages, or labor gaps is more useful than a polished capability presentation.
How Tube Makers Judge a Brand's Readiness for Custom Packaging
Tube makers rarely start with decoration. They start with whether a brand can answer basic technical questions about fill temperature, product pH, barrier requirements, and closure torque without scrambling. A company that walks in with those details plus a preferred tube diameter, orifice size, and seal type gets treated very differently from one that only knows it wants a nice look. That early clarity tells the manufacturer how many rounds of sampling the project will probably need.
Readiness also shows up in production expectations. Experienced suppliers listen for realistic talk about minimum order quantities, lead times, and print file formats. If a brand pushes for a full production run in two weeks or sends low-resolution artwork after the proof stage, it signals trouble ahead. Brands that lock artwork before requesting samples, understand the cost of plate changes, and have one person empowered to approve physical proofs tend to move through the line without unnecessary back-and-forth.
What a Short Run Reveals About a Partner's Real Standards
A short run has a way of stripping away the polite rehearsals people bring to dinner tables. Within the first ten minutes, pace becomes a quiet negotiation: one person sets a rhythm that feels effortless, while the other either adjusts without comment or lets the gap widen into a small, telling silence. What looks like exercise is really a compressed test of how someone handles mismatch, discomfort, and the need to cooperate when neither of you is at your best.
The details surface fast. A partner who notices you reaching for a slower cadence and matches it without being asked is showing a standard rooted in awareness rather than performance. Someone who repeatedly pushes the pace, then circles back with faint impatience, reveals whose comfort defines the shared plan. Even a question about an old knee or a worn shoe can expose whether care is an afterthought or an operating principle.
After the run, the conversation tends to reveal just as much. Does your partner focus on the route being too short, the weather being uncooperative, or the fact that you kept going when it got hard? The way they frame the experience often mirrors how they will treat larger shared challenges: not by the distance covered, but by whether you felt like an equal participant or an accessory to their pace.
Why Material Samples Matter More Than Digital Previews
A digital preview usually shows a material at its most flattering moment. The light is controlled, the angle is deliberate, and the color has been interpreted by a camera sensor and then again by your screen. What gets lost is how the surface actually responds when you tilt it, how the texture feels under a thumb, or how much warmer the tone becomes in late afternoon light. A physical sample removes that layer of guesswork because you are not looking at a version of the material; you are looking at the thing itself.
There is also a practical side that pixels cannot deliver. When you hold a sample, you can set it against existing furniture, flooring, or wall paint and watch how it shifts across the day. You notice the edge finish, the weight of the backing, and whether the sheen feels calm or slightly glossy in real conditions. Those details rarely survive compression and backlighting, but they are often the exact details that decide whether a choice feels right a month after installation.
Samples change the conversation as well. Passing a physical swatch to a client or contractor tends to focus attention on the actual object instead of a link that everyone opens on a different device. It cuts down on the familiar cycle of approvals based on mismatched screens and lets people agree on what is in front of them. The result is fewer surprises, fewer returns, and a decision that is grounded in handling rather than hoping.
The Difference Between a Vendor and a Partner on a Tight Deadline
When a deadline tightens, the difference between a vendor and a partner shows up in how they handle pressure. A vendor waits for instructions, completes the narrow scope, and disappears once the invoice is sent. A partner notices the parts of the project that are wobbling, asks about the unspoken risks, and adjusts their pace without being nudged. The vendor might deliver exactly what was ordered; the partner delivers what the moment actually requires, even if that means doing extra work that falls outside the original brief.
On a tight deadline, a vendor communicates in updates: status, percentage complete, next step. A partner communicates in judgments: what could break, what we can sacrifice safely, and where to spend the remaining hours. That difference becomes clearer around small failures. A vendor will point to the contract when something slips. A partner will already be offering a workaround, because they treat the goal as shared rather than borrowed. You don't need to manage a partner the way you manage a vendor; you can spend that energy on the parts of the project that still need decisions.
The real test isn't whether someone works fast. It's whether they carry part of the worried thinking with you. A vendor can be excellent at speed and still leave you holding every trade-off alone. A partner spreads the weight. Under a countdown, that difference is felt in the number of times you have to repeat yourself, chase a detail, or wonder if anyone else is watching the clock with the same urgency. One gives you a product on the last day. The other gives you options, warnings, and a sense that the deadline is being met together.
FAQ
Start with formula compatibility. Ask for barrier layer test data with fluoride, whitening agents, or high-menthol formulas. A tube that looks fine on a shelf can still cause flavor loss or active ingredient migration if the inner lining is wrong.
Have them explain the structure layer by layer, including where the EVOH or aluminum barrier sits and how thick it actually is. If they can also show accelerated stability results under heat and humidity, that is a much stronger signal than a polished sales pitch.
The good ones bring up shoulder sealing, orifice torque, and crimp integrity before you ask. They will also admit past production issues and explain what they changed. Vendors who only talk about capacity and low prices usually avoid the details that matter most.
Not necessarily. Some factories use low minimums to attract small brands but create consistency problems through frequent color changes and line swaps. Ask whether they have a dedicated small-batch line or documented cleaning procedures between runs.
A lot. Ask if they use dry offset or flexo, whether their inks have passed migration testing, and how they handle spot color matching. Real differences show up in fine text, gradients, and how the print survives crimping and repeated squeezing.
Go beyond the generic two-to-four week answer. Ask about capacity in peak periods like back-to-school or holiday promotions, and how they manage urgent orders. A good factory will share on-time delivery rates from the last several months without hesitation.
Push for specifics: what resin they use, what percentage of post-consumer recycled content is actually achievable in the tube body, and whether they have mass balance certification or third-party audit reports. Broad statements about recyclability are not enough.
Because a dimensional drawing cannot show you how the tube feels, how it springs back, or how the printed surface behaves after creasing. A reliable partner will send blank tubes first, then printed samples, so you can test under real filling and squeezing conditions.
Conclusion
Most custom toothpaste tube orders go sideways long before the first tube is extruded, and tube makers say the warning signs are usually hidden in the details brands overlook. A promising quote can fall apart when artwork files do not match the actual print repeat, when the declared tube diameter is off by a millimeter, or when nobody confirms how the barrier layer will behave with a particular fluoride formula. Before committing, it pays to ask uncomfortable floor-level questions about batch consistency, changeover discipline, defect sorting, and how the factory handles a short run without treating it as a nuisance. Experienced makers also gauge a brand's readiness by whether the team can answer basic fill-line questions: viscosity range, sealing temperature, cap torque, and expected fill speed. If those answers are vague, a capable partner will slow the process down and ask better questions instead of rushing to cut tooling.
Material samples tend to reveal what digital previews hide. A render will not show how a soft-touch laminate scratches after ten cycles in a travel bag, how the shoulder finish catches light, or how the tube springs back after squeezing. Likewise, a short run is more than a cost-saving test; it exposes edge trimming, cap alignment, and sealing consistency that only show up when the line is actually running. Tight deadlines make the difference between a vendor and a partner obvious. Vendors quote quickly and disappear when a delay appears. Partners surface trade-offs early, adjust artwork or filling specs without drama, and keep the project moving. Packaging partners worth keeping are the ones who treat a brand's constraints as part of the design brief rather than an excuse for mediocrity.
Contact Us
Contact Person: Alex Wu
Email: [email protected]
Tel/WhatsApp: 86-20-37965868
Website: https://www.gzsanrong.com/en.html