Wholesale D Rings Bulk Buying Guide and Key Considerations
2026-10-06
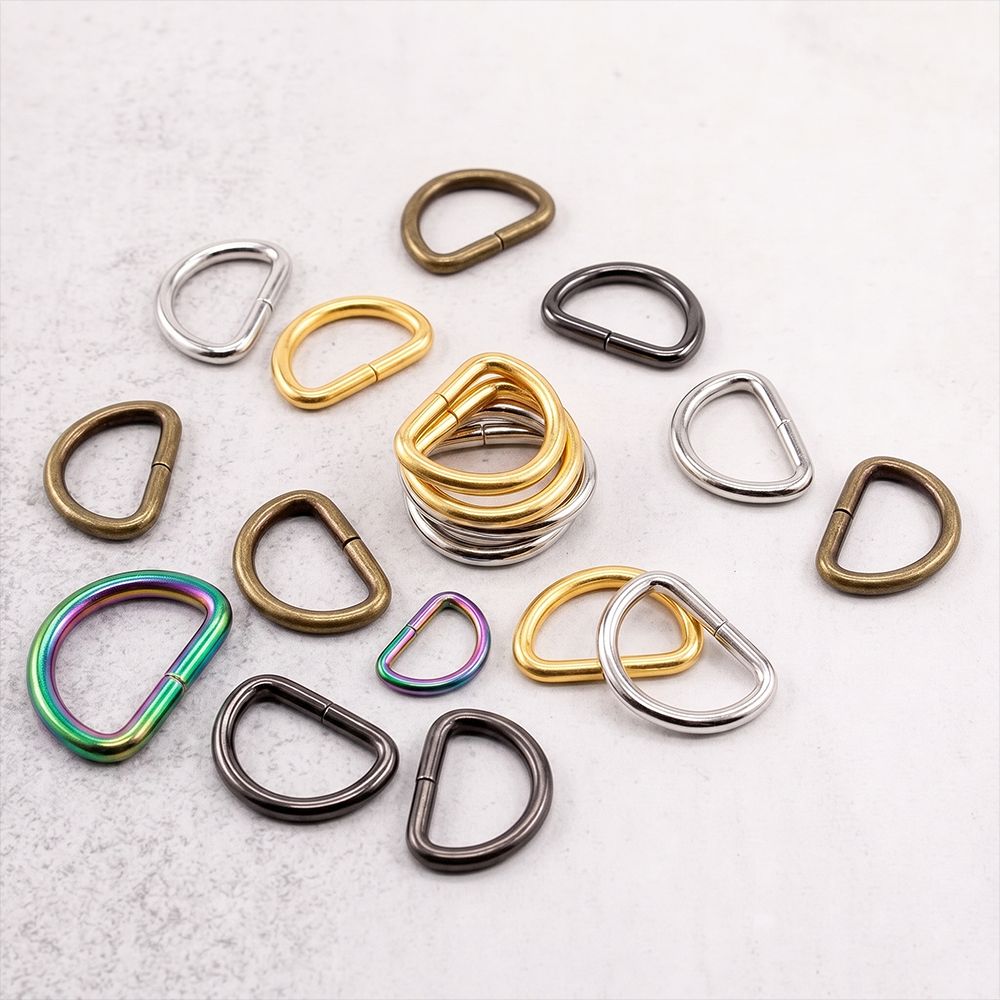
Most buyers don't realize that not all D rings are created equal—until a batch fails under load. If you're planning a bulk order, understanding the subtle differences in gauge, coating, and load rating can save you from expensive rework and delays. This guide walks you through what actually matters when buying wholesale D rings, so you can make confident decisions. For hardware that consistently passes inspection, Kingming offers a range worth checking out.
Material Choices Shape Both Price and Performance
Material choices are rarely just a matter of cost; they set the boundaries for what a product can do. Take bicycle frames: an aluminum alloy keeps the price accessible and delivers crisp, efficient power transfer, but it transmits every road vibration straight to the rider. Carbon fiber, by contrast, can be laid up to soak up chatter while remaining laterally stiff, yet that comfort and tuning come at a noticeably higher price and a more fragile impact profile. The same trade-off shows up in kitchen knives, where high-carbon stainless steel holds an edge longer than softer alloys but demands more careful maintenance to avoid chipping or rust.
Sometimes the smartest material decision isn't the most exotic one. A well-chosen engineering plastic can outperform metal in certain wear situations, reducing both weight and manufacturing cost without sacrificing lifespan. Conversely, paying for titanium in a watch case or eyewear frame often buys corrosion resistance and a featherlight feel, but those benefits may be invisible to buyers who only compare spec sheets. Understanding where materials earn their premium helps separate genuine performance gains from marketing gloss.
The balance between price and performance also shifts with production volume and intended use. For a one-off prototype, machining a part from billet aluminum may be cheaper than tooling up for injection molding, even if the per-unit cost would be higher at scale. In mass-market goods, a small change in alloy composition or polymer grade can trim pennies per unit while subtly changing durability, heat tolerance, or tactile quality. Reading those material choices is a way to see what the manufacturer prioritized—and what they quietly accepted as a compromise.
Weight Ratings Are Not a Suggestion
Many lifters treat the numbers printed on weight plates as rough guidelines rather than hard limits, but that mindset quietly undermines progress. A ten-pound plate is not an estimate; it is ten pounds of resistance demanding your muscles adapt. When you casually add “about five more” or skip the last pair because it feels close enough, you rob yourself of measurable overload. Small discrepancies accumulate into plateaus that feel mysterious but are actually the predictable result of inconsistent loading.
Precision in weight selection also protects your joints and connective tissue. A sudden jump from 135 to 155 because the 145 wasn’t “worth the hassle” loads your tendons beyond their current capacity. Conversely, believing you lifted 200 when the bar actually weighed 195 creates a false sense of achievement. The rating exists because steel has no opinion. Your training log, on the other hand, should reflect reality, not your mood that day.
Treat every increment as a deliberate choice. If the program calls for 72.5 pounds, find the fractional plates or use a change plate system. If you cannot load the exact weight, adjust reps or tempo instead of pretending the number doesn’t matter. Progression lives in the gap between what you lifted last week and what you lift this week—and that gap is only real when the numbers are honest.
Electroplating, Powder Coating, or Bare Metal?
Choosing between electroplating, powder coating, and leaving metal bare rarely comes down to a simple checklist. Each finish carries its own personality under real-world conditions, and what looks ideal in a catalog often behaves differently once temperature swings, moisture, or repeated handling enter the picture. Electroplating adds a metallic skin—nickel, chrome, zinc—that can boost conductivity or corrosion resistance, but the bond is only as good as the surface prep and the bath chemistry on a given day. Powder coating, by contrast, wraps the part in a thick, cured polymer layer that shrugs off scuffs and chemicals, yet it can hide fine details and alter dimensional tolerances. Bare metal, often dismissed as unfinished, actually offers unmatched authenticity and repairability, provided the alloy can survive its environment without pitting or oxidizing.
The decision gets more interesting when you consider how the part will be touched, cleaned, or inspected over its service life. A handrail in a coastal building might look elegant in brushed stainless steel, but constant salt spray could turn that bare surface into a maintenance headache; a thin electroplated layer might fare even worse if scratches expose the base metal. Powder coating would excel there, though the same coating on a precision bracket could throw off assembly clearances by a few crucial microns. Meanwhile, a heatsink or grounding component may need the direct metal-to-metal contact only bare or electroplated surfaces can provide, making powder coating a non-starter despite its durability.
Rather than framing this as a hierarchy, it helps to ask which failure mode you can live with. Bare metal fails visibly—rust, tarnish, wear—but it can be refinished indefinitely without stripping old coatings. Electroplating fails subtly, often from porosity or edge thinning, and rework usually means stripping and replating the entire piece. Powder coating fails by chipping or fading, but its damage tends to stay localized and can sometimes be touched up in the field. The best choice often depends less on the material itself and more on who will maintain it, what they can tolerate, and whether the part's function depends on its surface being conductive, insulated, or simply honest about what it is.
Ordering in Bulk: When Discounts Actually Start
Most people assume that ordering more units automatically unlocks a bigger discount, but the reality is messier. Suppliers often use tiered pricing, and the sweet spot rarely sits at the maximum quantity. Take a typical pricing sheet: 100 units at $10 each, 500 at $8, 1,000 at $7.50, and 2,000 still at $7.50. The per-unit price stops moving after 1,000, so that extra 1,000 units just adds storage headaches without any additional savings. The discount doesn't "start" at some magic number—it plateaus, and smart buyers learn to spot the flat part of the curve early.
Then there are the hidden costs that eat into bulk discounts. Warehousing, insurance, and the risk of obsolescence or spoilage all rise with volume. A 12% price break for ordering a year's supply sounds great until you figure out that holding that inventory costs you 6% of its value annually. Suddenly your real discount is more like 5%, and you're tying up cash that could be earning interest elsewhere. The true start of a meaningful discount is when the net savings—after all carrying costs—actually justify the larger order, not just when the sticker price drops.
Instead of chasing the biggest volume, pull the supplier's full tier chart and calculate total cost of ownership at each level. Sometimes the best deal is a smaller quantity with free shipping or a waived setup fee, which is effectively a discount that doesn't show up in the unit price. Watch how the per-unit cost changes between tiers, not just the total invoice. If the drop from 800 to 1,200 units is only 2%, but the drop from 500 to 800 is 9%, the discount has already started—and mostly finished—before you ever hit the top bracket.
Supplier Red Flags You Can Spot Early
A supplier who dodges your questions about production capacity, lead times, or past client references isn't just being vague—they're waving a flag you can't afford to ignore. Early conversations should feel like opening a window, not pulling teeth. If every answer comes wrapped in “trust me” or “we'll handle it later,” you're not looking at a partner; you're looking at a future bottleneck.
Another telltale sign hides in the paper trail. Invoices with mismatched numbers, contracts that shift terms between drafts, or quality certificates that expire suspiciously soon—these aren't clerical oversights, they're patterns. A supplier who can't keep their documentation straight before you've signed a purchase order will only multiply the chaos once your inventory depends on them.
Watch also for the overpromiser. If a supplier claims zero defects, 24-hour turnaround on custom orders, and the lowest price you've ever seen, one of those promises is already broken. Early red flags rarely announce themselves as failures; they show up as too-good-to-be-true consistency. Ask for a small trial order, a sample batch, or a walkthrough of their last client's onboarding. The response—or the hesitation before it—will tell you more than any brochure.
From Sample to Shipment: A Practical Inspection Plan
Getting a product from an approved sample to the loading dock without quality slip-ups isn't about luck—it's about checking the right things at the right stages. Many teams skip the middle ground between "we loved the prototype" and "the container is sealed," only to find out later that a material swap or a rushed production line quietly changed what the customer actually receives. A practical inspection plan bridges that gap by treating each phase as a filter, not a hurdle.
Start with the golden sample as your reference point, but don't assume the factory will naturally match it. During the raw material and first-off inspection, compare every critical component—fabric weight, seam strength, electronic tolerances, color under daylight—against that sample, not against a vague spec sheet. Then move to an inline check when roughly 20-30% of the order is finished, because that's when you can still correct course without scrapping everything. Finally, a pre-shipment inspection right before packing and sealing acts as your last line of defense, focusing on quantities, labeling, packaging, and a second look at defects that may have slipped through earlier.
Make the plan realistic by choosing random sampling based on batch size, not just checking the first few cartons. And document findings with photos and simple checklists rather than lengthy reports nobody reads. The goal isn't to produce paperwork—it's to catch the difference between what was promised and what's about to leave the factory, before your customer does.
FAQ
Most bulk D rings are made from zinc alloy, stainless steel, or solid brass. Zinc alloy is cost-effective and fine for lighter use, but it can corrode if the plating wears off. Stainless steel holds up much better outdoors and in wet conditions, especially marine-grade 304 or 316. Brass has a classic look and resists rust, though it costs more and may tarnish without a clear coat.
Ask the supplier for a breaking strength or safe working load rating rather than guessing from the size. A welded stainless steel D ring might hold several hundred pounds, while a cast zinc ring of the same width could snap under moderate tension. Match the rating to your worst-case use, not the average, and add a safety margin of at least two to three times the expected load.
Common finishes include electroplated nickel, matte black, antique brass, and raw or polished metal. Electroplating is fine for fashion accessories but can chip quickly on gear that gets rubbed or dropped. Powder coating tends to hold up better on steel rings used outdoors. If you want a metallic look without rust, choose stainless steel instead of relying on a coating over zinc.
There's no universal standard, so base the inner width on the strap or webbing you plan to thread. For a 1-inch strap, a D ring with a 1.25-inch inner width gives enough room to move freely without jamming. For thicker padded straps or multiple layers, add half an inch or more. Always ask for a physical sample before committing to a large order.
It depends on the supplier and whether you choose a stock size or a custom design. Many factories and importers start at 1,000 pieces per size and finish for stock items, while custom molds can require 5,000 to 10,000 pieces or more. Smaller distributors may sell packs of 100 or 500 at a higher unit price, which can work for testing a market.
Request a pre-production sample, then order a small trial batch before the full run. Compare the weight, finish, and dimensions against the approved sample. Ask the supplier to provide a written inspection report or hire a third-party inspection service for the final shipment. Check for sharp edges, uneven plating, mismatched inner widths, and weak weld points.
Imported rings from countries like China or Taiwan often cost less per piece, especially for zinc and brass, but lead times and shipping can be longer. Domestic suppliers usually offer faster turnaround and easier communication, which helps if you need smaller batches or quick reorders. Balance the landed cost per piece against the risk of delays and the value of being able to reach someone by phone.
Beyond the unit price, watch for tooling fees on custom shapes, plating surcharges for small lots, shipping weight charges, import duties, and potential rejection losses if a batch arrives below spec. Some suppliers quote a low base price but add fees for packaging, labeling, or metal certification. Ask for a complete landed-cost breakdown before comparing offers.
Conclusion
Material choice is first thing that separates a usable D-ring from one that bends under load. Zinc alloy might be fine for lightweight straps or pet accessories, but forged carbon steel or stainless holds up when the ring is pulling against webbing, hardware, or human weight. Don't just look at the metal type—check how it was formed. Cast rings are cheaper but can have hidden porosity; forged or stamped options tend to be more consistent. Weight ratings are printed on spec sheets for a reason. If a supplier can't tell you the breaking strength or working load limit, that's a problem. Also, finish matters more than appearance. Electroplating adds a thin layer but can flake if the base metal is rough; powder coating offers a thicker, more even coat for outdoor or high-wear use; bare metal is only acceptable when you're handling corrosion elsewhere or want a raw industrial look that will age.
Bulk pricing doesn't magically start at 500 pieces. Many factories offer a real break at 1,000 or 2,000 units, but before you commit, ask for a tiered quote and compare landed cost, not just unit price. Early supplier red flags include vague answers about tolerances, unwillingness to share a mill certificate, or photos that look stolen from another catalog. A practical inspection plan is non-negotiable: order a pre-production sample, check dimensions and finish under normal light, then pull random pieces from the first mass production run before shipment. Don't accept a sample that was hand-picked and polished separately from the batch you'll actually receive. If the supplier pushes back on third-party inspection or tries to rush you past the sample stage, walk away.
Contact Us
Contact Person: Jamie Zeng
Email: [email protected]
Tel/WhatsApp: +86 13728219269
Website: https://www.kmhardware.com